High-efficiency components designed for smart infrastructure, edge computing nodes, and advanced illumination systems.
Pioneering High-Performance Semiconductor and Smart Manufacturing Excellence Since 2017
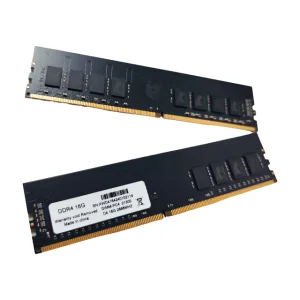
Velmix Technology Co., Ltd. is a professional DDR5 memory manufacturer based in Shenzhen, China, specializing in the research, development, production, and global distribution of high-performance DRAM memory solutions. Since its establishment in 2017, Velmix has been committed to delivering reliable, high-speed memory products for consumer electronics, industrial applications, gaming systems, servers, and embedded computing.
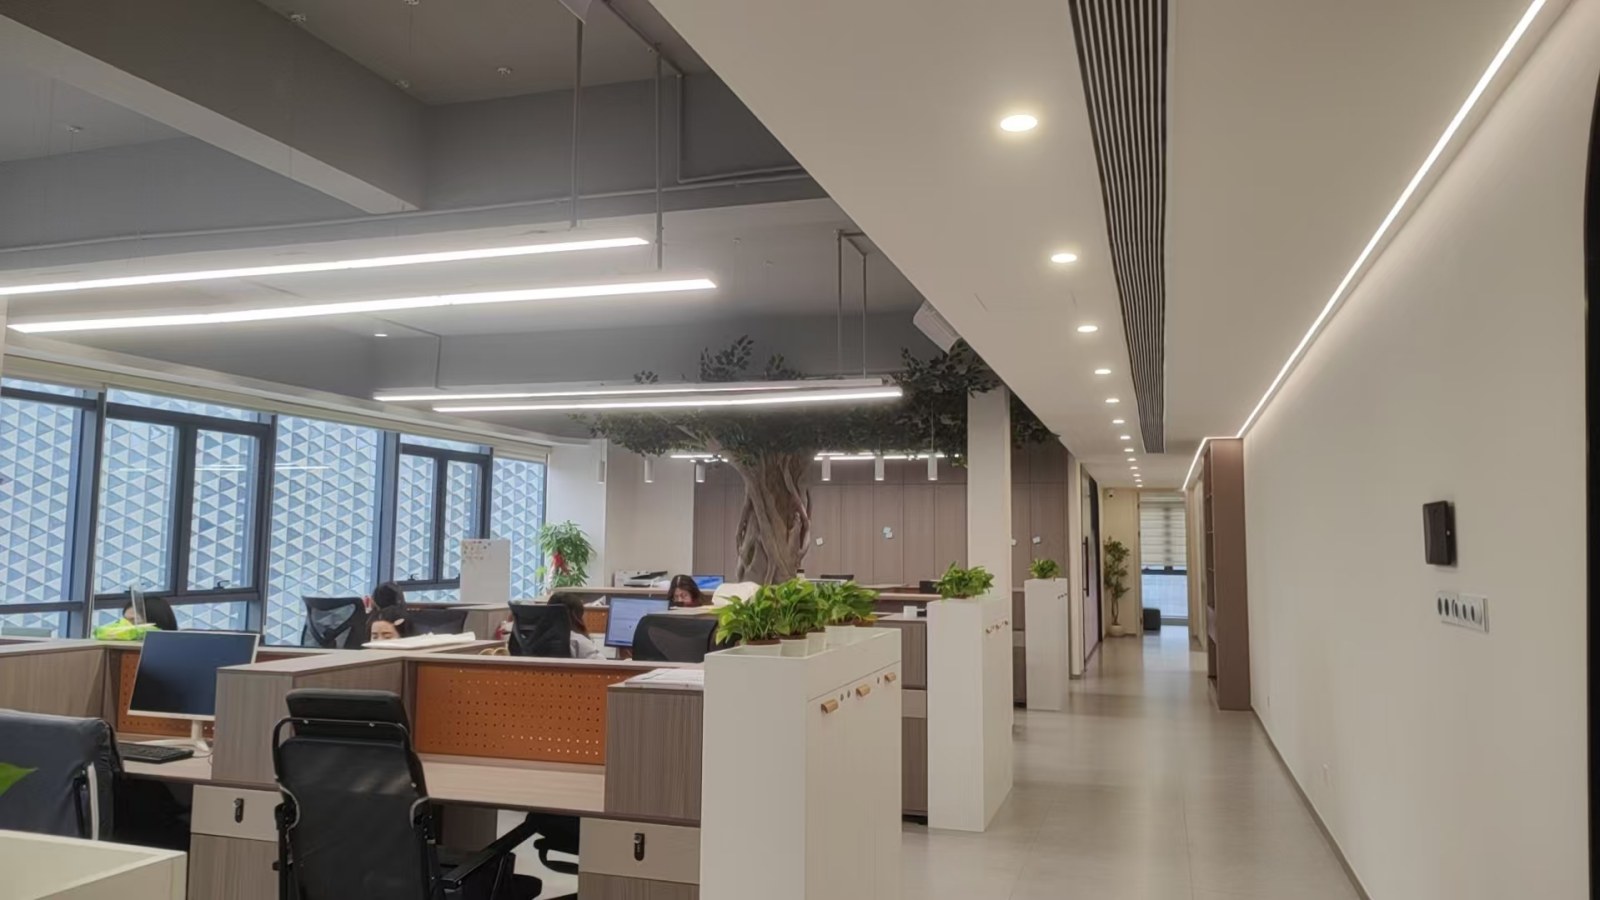
Operating from a modern manufacturing facility covering 368㎡, we combine advanced production technologies with strict quality management to ensure every memory module meets international performance and reliability standards. Our experienced engineering team continuously develops innovative DDR5 memory solutions to meet the evolving demands of AI computing, edge devices, cloud infrastructure, and next-generation computing platforms.
Today, Velmix serves customers in more than 40 countries and regions, offering flexible OEM and ODM manufacturing services for global brands, distributors, system integrators, and industrial equipment manufacturers. By focusing on product consistency, fast delivery, and technical innovation, we have built long-term partnerships across Europe, North America, Southeast Asia, and the Middle East.
| Item | Information |
|---|---|
| Company Name | Velmix Technology Co., Ltd. |
| Established | 2017 |
| Facility Area | 368㎡ |
| Annual Export Revenue | USD 18.6 Million |
| Export Experience | 8 Years |
| Industry Experience | 15 Years |
| Quality Control | 100% Full Inspection Before Shipment |
| Product Inspection Methods | Signal Integrity Test, Burn-in Test, Compatibility Test, Functional Test & Random Sampling |
| QC Staff | 56 Employees |
| Business Type | Manufacturer & Exporter |
| Main Markets | North America, Europe, Southeast Asia, Middle East & South America |
| Supply Chain Partners | 986+ |
| Main Customer Types | Brand Owners, OEM Manufacturers, System Integrators, Distributors & Wholesalers |
| R&D Capability | Independent Product Design, PCB Development & Firmware Optimization |
| Customization Options | OEM, ODM, Private Label, Customized Capacity, Heat Spreader, PCB Color & Packaging |
| New Products Launched Last Year | 138 Models |
| R&D Engineers | 84 Engineers |
Driven by innovation, precision manufacturing, and customer-oriented service, Velmix continues to expand its portfolio of DDR5 memory products while helping global partners build faster, more reliable, and more efficient computing systems. We are dedicated to becoming a trusted long-term supplier of premium memory solutions for customers worldwide.
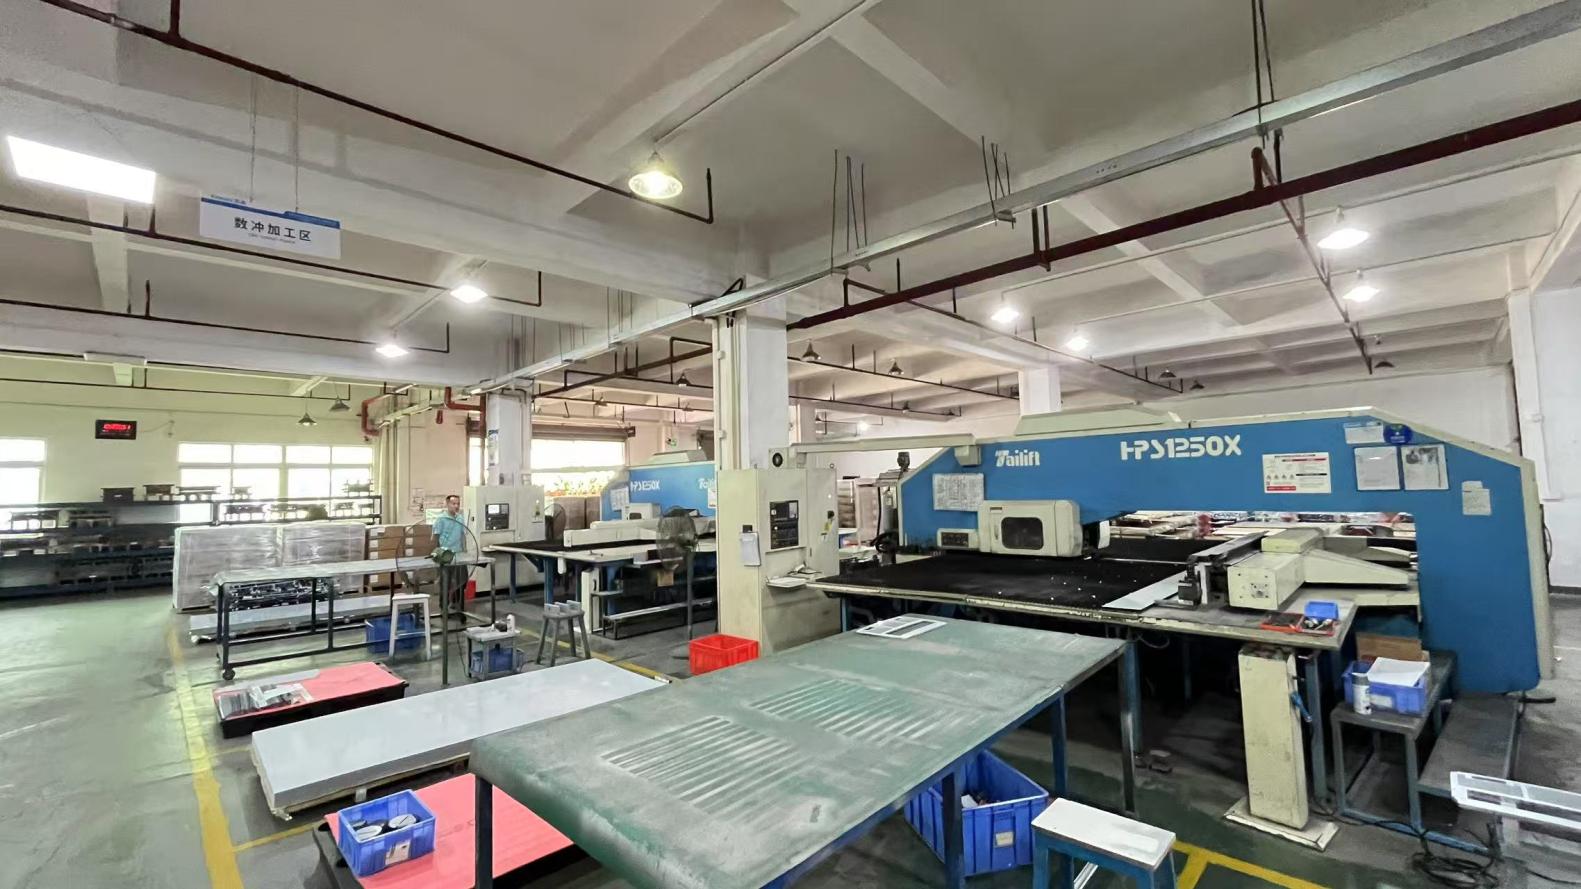
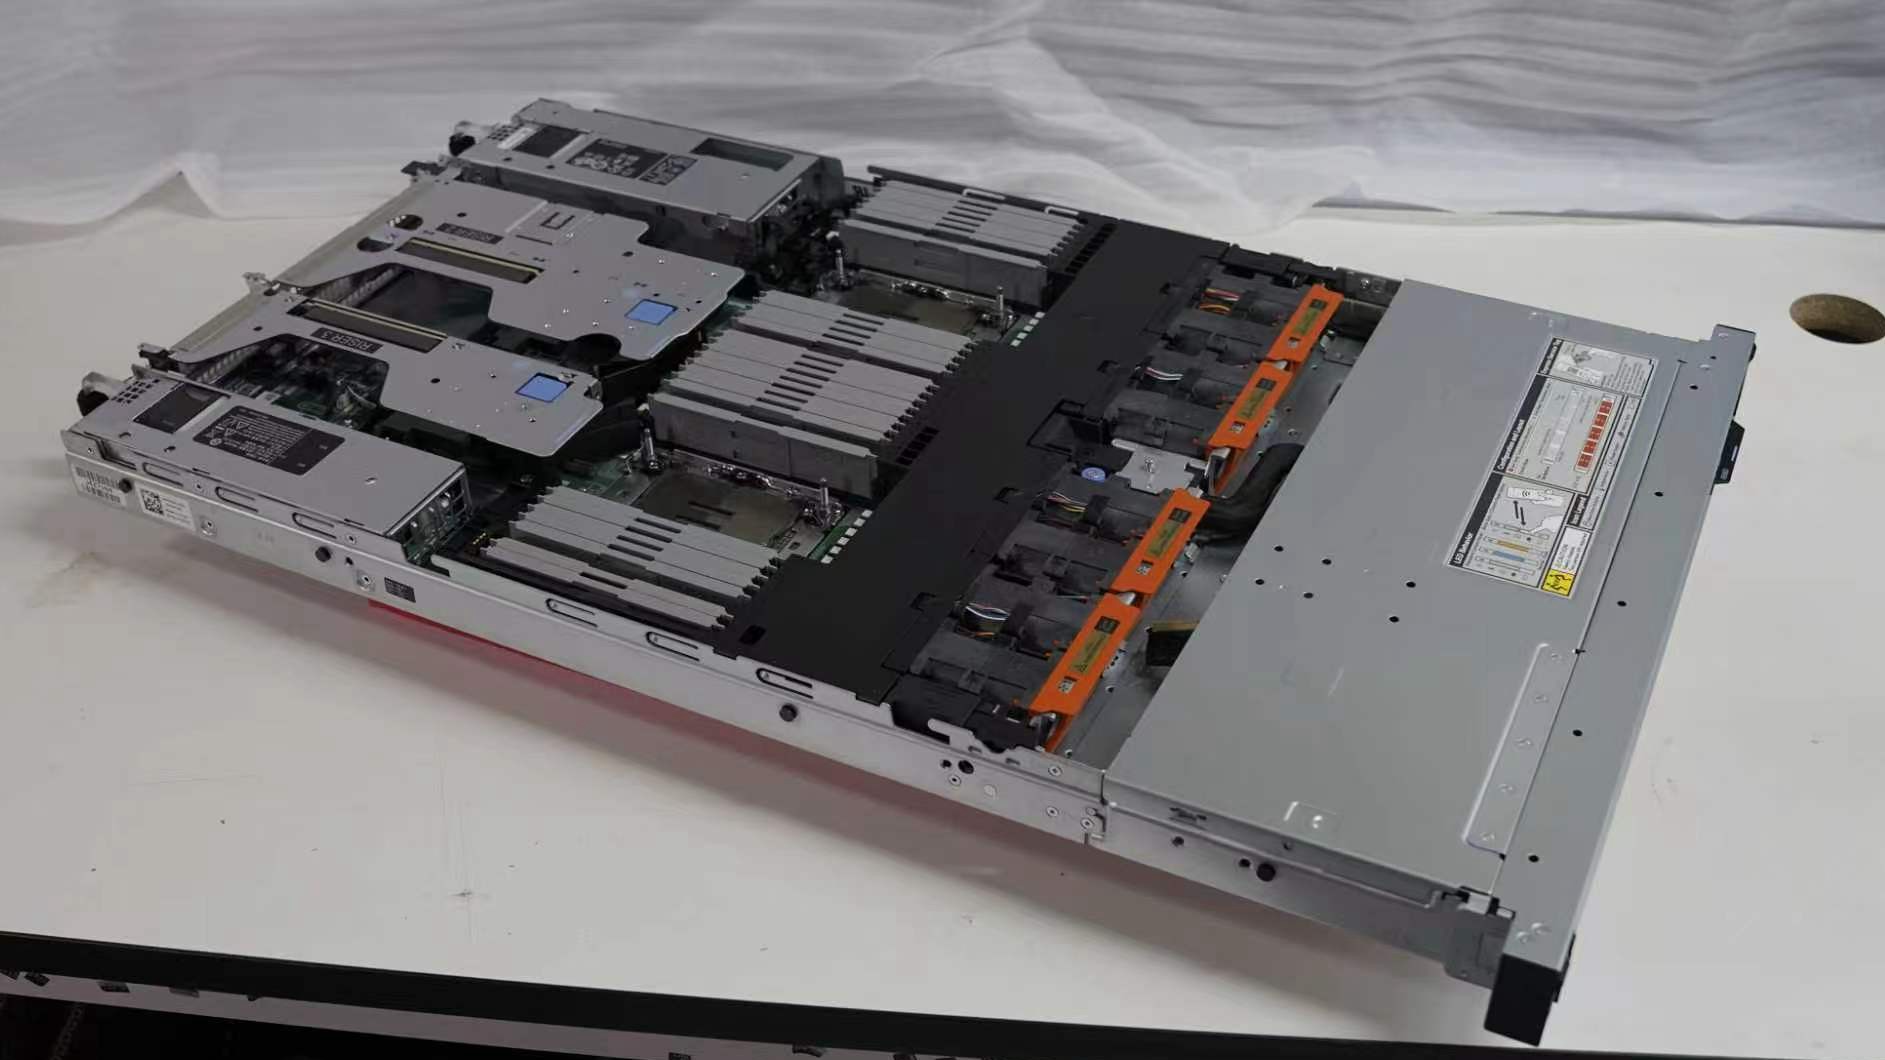
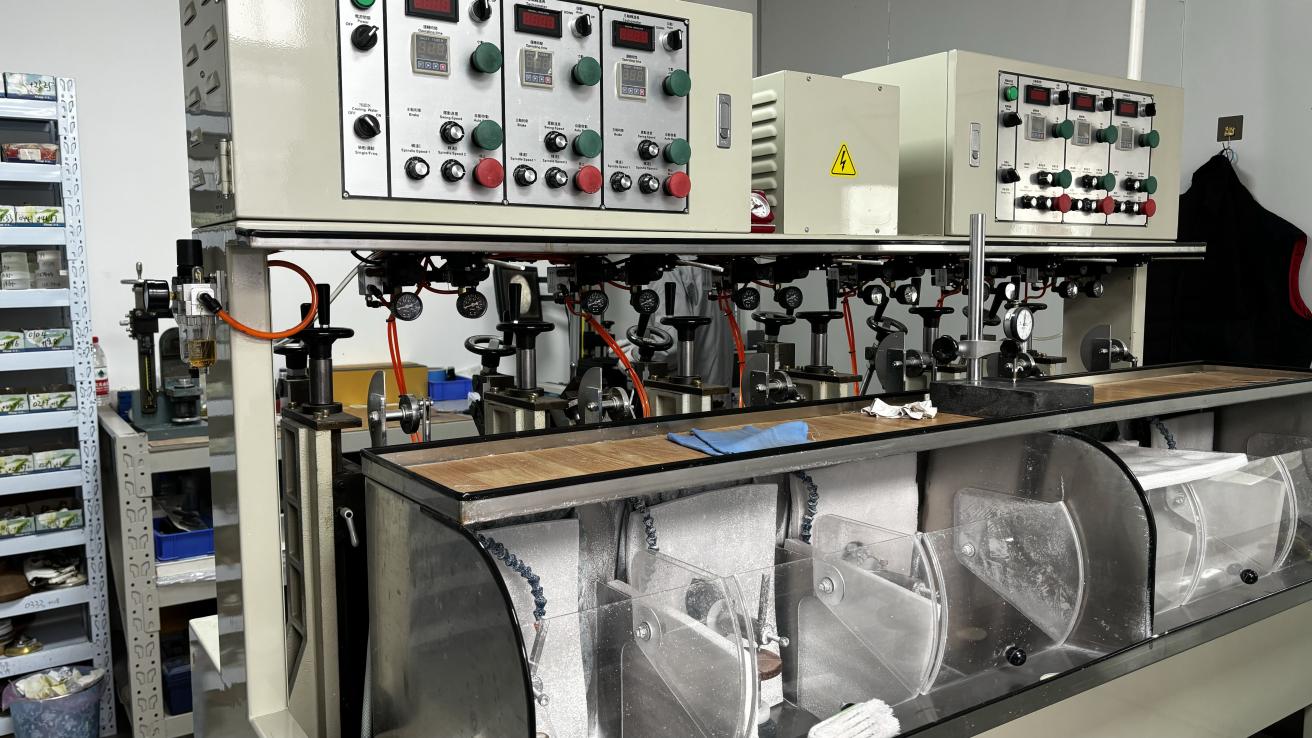
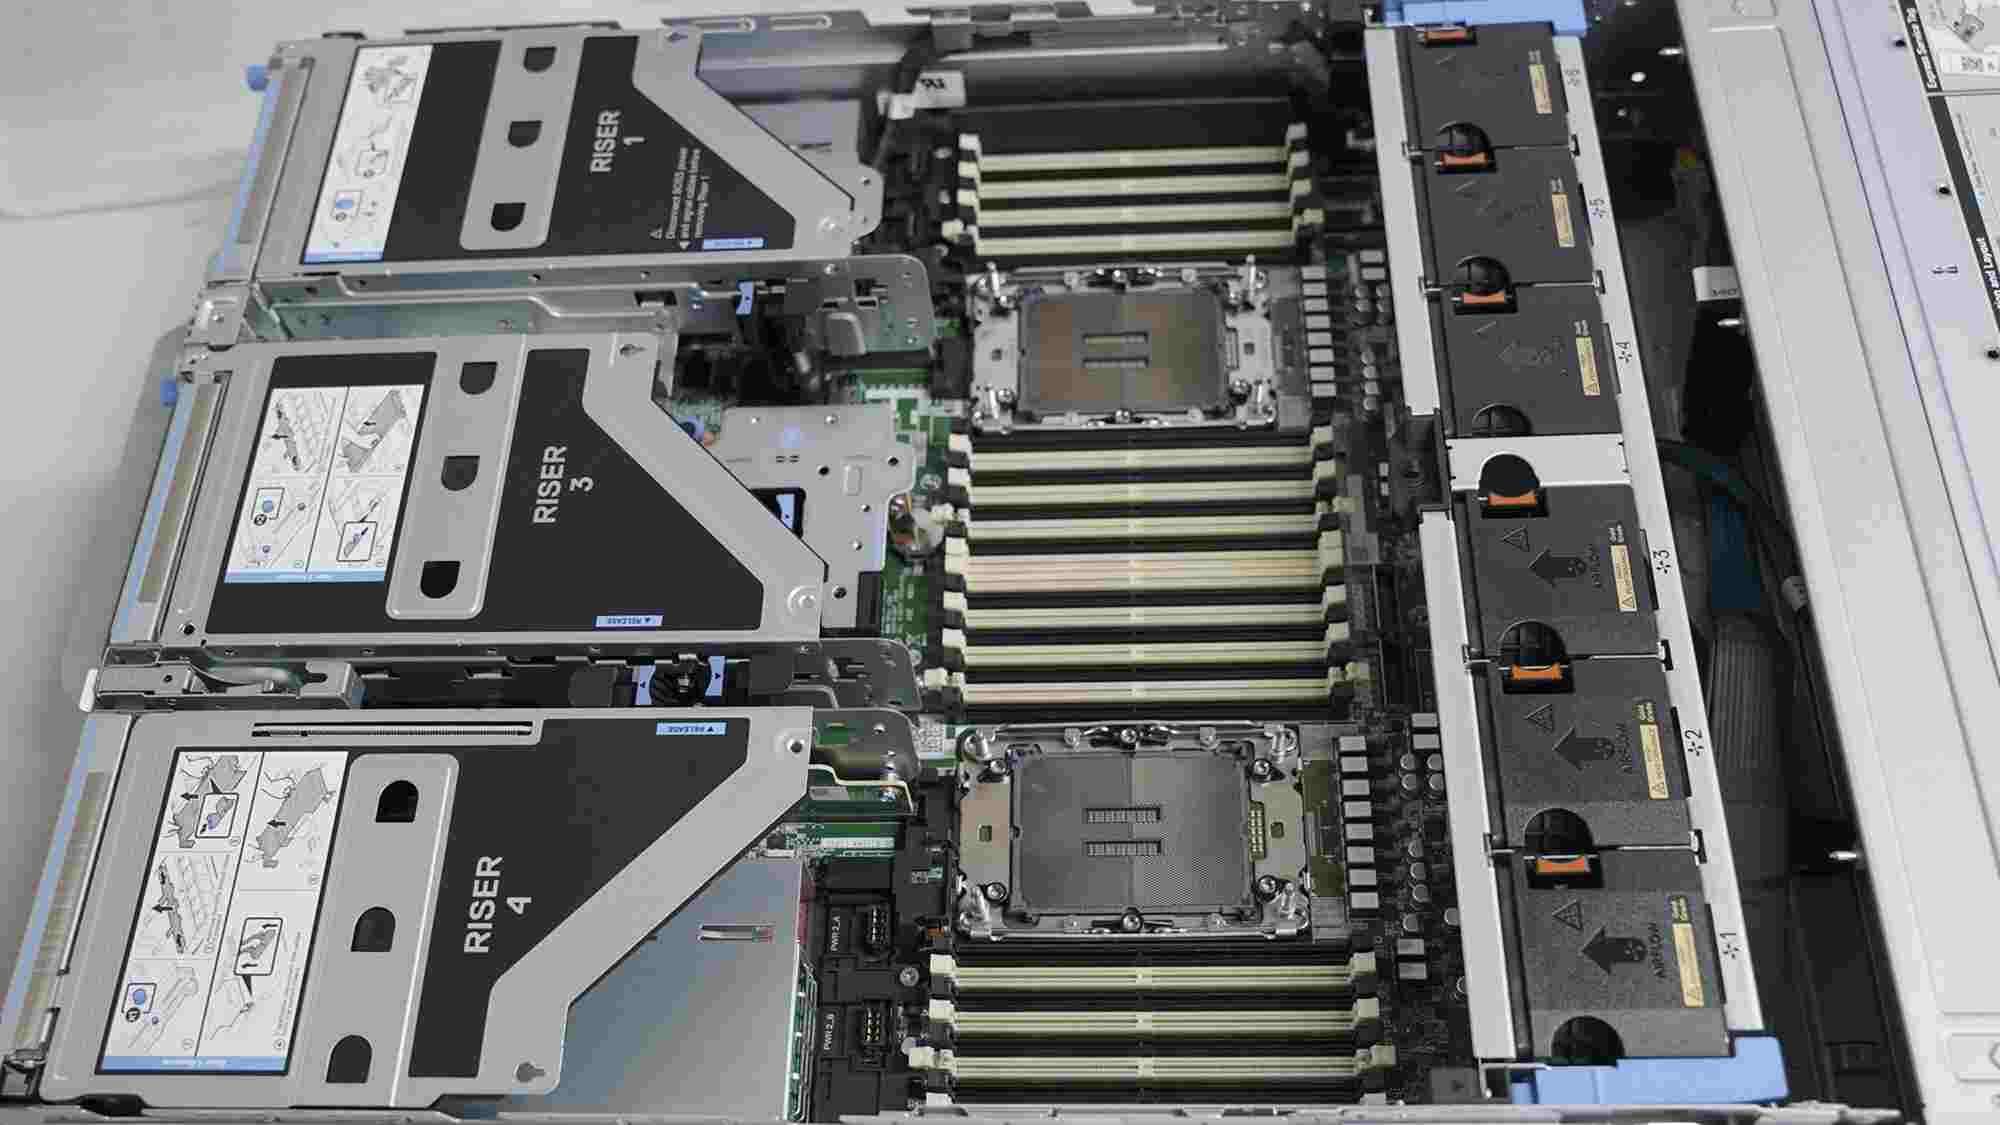
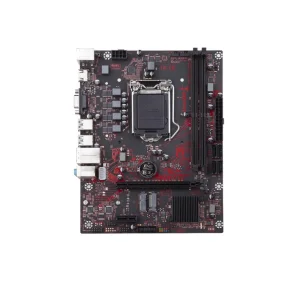
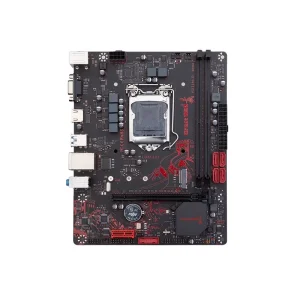
Precision-engineered motherboards and thermal cooling assemblies ensuring supreme stability for high-load systems.
An authoritative analysis of technical roadmaps, localization compliance, and supply chain efficiencies for CE Certified Smart Light Bulbs.
Smart light bulbs are no longer isolated residential novelties; they form the bedrock of localized smart city infrastructure and intelligent commercial complexes. In residential automation, integration with voice assistants (Alexa, Google Assistant, Apple HomeKit) via Zigbee 3.0 and Matter protocols enables adaptive circadian lighting.
In commercial and industrial sectors, networked smart bulbs equipped with ambient light sensors and occupancy detection reduce facility energy consumption by up to 45%. Our CE-certified architecture ensures seamless compatibility across European 220V–240V grids and diverse regional wireless frequencies.
The next decade of smart illumination points toward Edge AI integration and Li-Fi data transmission capabilities. Our R&D division is actively embedding micro-neural processors directly into driver ICs, allowing smart bulbs to execute local facial recognition and behavioral analytics without cloud latency.
Furthermore, the adoption of Matter IoT standards guarantees cross-platform interoperability, eliminating vendor lock-in and securing long-term enterprise scalability for global distributors and system integrators.
Positioned in Shenzhen’s core electronics manufacturing hub, Velmix leverages an agile supply chain comprising over 986 certified upstream partners. This vertical integration guarantees raw material stability, rapid prototyping turnaround, and strict cost competitiveness.
Our automated SMT assembly lines and rigorous QA protocols—including burn-in testing and signal integrity verification—ensure that every batch shipped to North America, Europe, and Southeast Asia maintains a near-zero defect rate.
Global export success relies heavily on rigorous regulatory adherence. All our smart lighting and hardware offerings carry mandatory CE, RoHS, and FCC certifications. We provide comprehensive documentation packages, EMC test reports, and customized regional packaging to ensure frictionless customs clearance and legal compliance in target international markets.
Expert answers regarding our manufacturing capabilities, certifications, and global export services.
 Velmix