A memory module looks simple from the outside: a narrow circuit board, several black chips, and a small identification label. Its reliability, however, depends on careful choices at every production stage. This guide explains the Memory module manufacturing process, from selecting compatible DRAM chips and designing the printed circuit board to surface-mount assembly, firmware programming, testing, and packaging. Small details matter. A misplaced component or weak solder joint can cause failures that appear only under demanding workloads.
Gordon Moore, Intel co-founder and semiconductor pioneer, famously observed, “The number of transistors incorporated in a chip will approximately double every 24 months.” His statement concerns chip development, not a specific module factory. Still, it helps explain why manufacturers must continually adapt their designs and quality checks. In practice, production involves more than placing chips on a board. Engineers verify component compatibility, control assembly temperatures, and test modules for capacity, speed, and stability. Results can vary with equipment, materials, and product specifications. That part is easy to overlook. This introduction sets out the major steps, the purpose of each inspection, and the practical issues that shape dependable memory modules. No process is flawless; understanding where errors can occur is part of making better products.
A DDR5 DIMM design begins with its 288-pin connector and the motherboard socket it must fit. Those pins carry data, power, ground, and control signals, so the layout cannot treat them as interchangeable. Measure twice. The module also divides its data interface into two independent 32-bit subchannels, rather than one 64-bit channel. This lets the memory controller manage separate data requests more flexibly.
That split shapes the circuit board. Designers place memory packages on both sides when the module layout allows it, then route each subchannel’s signals with carefully controlled spacing and length. A trace that runs too close to a noisy power path can weaken signal quality. Tiny details matter. The board’s layer stack, copper thickness, and connector contacts all affect electrical behavior, so engineers review simulations before releasing manufacturing files.
In production, automated equipment places components onto the board, and soldering secures them in place. Inspection checks for shifted packages, incomplete joints, and surface defects. Testing then verifies that both subchannels communicate reliably across supported speeds and operating conditions. A clean schematic is not enough; real boards can expose routing assumptions that looked harmless on screen. That lesson is easy to overlook. Teams may need to revise the layout after test results reveal a weak signal margin.
A memory module depends on more than fast components. Its multilayer PCB must carry high-speed signals with predictable impedance, even through tight spaces around memory chips. That starts with a carefully planned stackup. Engineers select core and prepreg thicknesses, copper weights, and dielectric properties to match the routing requirements. Small changes matter.
Signal traces are then designed with controlled width and spacing. Reference planes beneath them provide a consistent return path and help limit noise. For differential pairs, matched lengths and steady spacing reduce skew. Avoiding abrupt bends, unnecessary vias, and long stubs can also protect signal quality. The layout may look tidy, but appearance alone proves little.
During fabrication, lamination pressure and temperature can affect dielectric thickness, so process controls matter. A test coupon built alongside the board gives technicians a practical way to check impedance, often with time-domain reflectometry. Results should be compared with the design target and the agreed tolerance. On a production floor, measurements can reveal issues that a layout review misses. Still, one coupon cannot represent every detail of a finished module; that limitation deserves attention. Careful documentation of materials, stackup, and test results makes later troubleshooting more reliable.
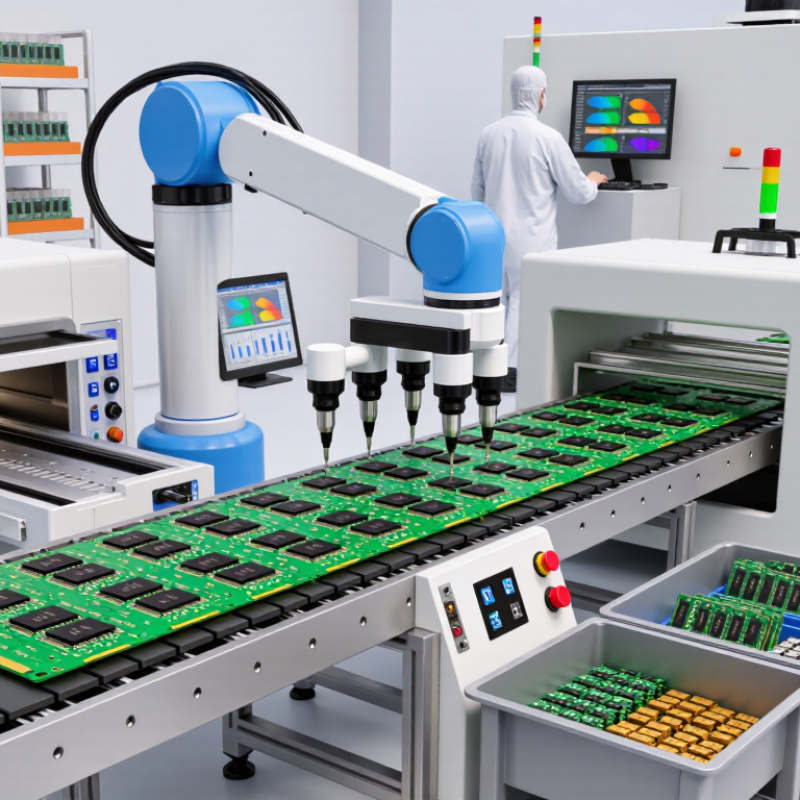
Memory module assembly begins with a clean, dry PCB and a verified solder-paste stencil. The paste deposits must be even, especially beneath fine-pitch SPD Hub and PMIC packages. DRAM packages often use dense ball-grid arrays. Small details matter.
A placement machine aligns each component to its board pads, but inspection remains essential. Reflow profiles should match the solder alloy, board design, and component limits. Track the ramp rate, peak temperature, and time above liquidus with thermocouples on representative boards. Too much heat can stress packages; too little can leave weak or incomplete joints. There is no safe universal profile.
After cooling, automated optical inspection checks visible alignment and solder defects. X-ray inspection can help assess hidden joints beneath DRAM packages, though it cannot replace electrical testing. The SPD Hub should be programmed and verified according to the module specification. Test PMIC output rails, memory continuity, and module operation under controlled conditions. A board may look flawless and still fail at startup. That is an important reminder: inspection results need functional evidence. Small process variations can matter. A slightly uneven paste deposit, for example, may cause intermittent contact that appears only during testing. The manufacturing record should preserve placement, reflow, inspection, and test data for traceability.
During memory-module manufacturing, SPD programming records the module’s supported data rates, timings, organization, and operating parameters. JEDEC’s JESD300-5 standard describes DDR5 Serial Presence Detect contents, while JESD79-5C specifies DDR5 electrical requirements. It lists 1.1 V as the nominal VDD and VDDQ supply, with a separate 1.8 V VPP supply. Keep those rails distinct. A correct SPD profile cannot compensate for unstable power delivery.
A practical verification station should write the intended profile, read it back, and compare key fields against the production record. Then test each module at its rated settings and measure VDD and VDDQ close to the socket under load. A bench reading at idle may miss brief voltage droop. Record the measurement conditions, instrument accuracy, and temperature; otherwise, results are hard to reproduce. JEDEC’s stated nominal voltage is a reference, not a substitute for checking the applicable tolerance and test limits. A rushed fixture can lie.
Tips: Verify SPD data before thermal testing. Use a calibrated meter or oscilloscope, and check probe placement. Retest samples after rework. Small process variations matter, and sometimes the test setup—not the module—is the weak link.
DDR5 nominal supply rails provide a useful reference when programming and checking module SPD data. These are nominal values, not production measurements.
DDR5 DRAM core (VDD) and I/O (VDDQ) nominal supplies are 1.1 V; VPP and the SPD hub supply (VDDSPD) are nominally 1.8 V. Confirm the module’s SPD profile and verify its supply rails against the applicable component and module specifications.
At 4,800 MT/s and above, memory-module validation must go beyond confirming that a system boots. Each module should be checked for usable capacity, correct data organization, and stable operation across supported voltage and temperature ranges. Labels prove little. Test every production lot with calibrated equipment, and retain traceable results for each sample.
Timing tests should examine more than a single pass or fail. Verify read and write behavior, command timing, refresh intervals, and training margins under realistic workloads. Then inspect signal integrity at the intended data rate. Eye diagrams can reveal reduced voltage or timing margin; probing near the module connector may expose reflections, crosstalk, or ringing. Small layout or fixture differences matter. Margins matter. Keep cables short and fixtures consistent.
Repeat tests after thermal soak and across multiple units, not just a hand-picked sample. Compare results against defined limits, and investigate gradual margin loss before it becomes a field failure. A module may pass once and still be fragile. It is tempting to accept a narrow margin after a pass; that judgment deserves a second review. Measurement uncertainty is real, and sometimes the fixture is the problem. Document the setup, calibration date, firmware, and environmental conditions so another engineer can reproduce the result.
It helps high-speed signals travel with predictable electrical behavior. Reference planes provide a steadier return path and can reduce noise.
Stackup thickness, copper weight, and dielectric properties all matter. Trace width, spacing, matched differential pairs, and via placement also influence performance. Small changes count.
A test coupon can be measured with time-domain reflectometry. Technicians compare results against the design target and agreed tolerance. One coupon is not the whole board.
The profile should suit the solder alloy, board, and component limits. Excess heat can stress packages; insufficient heat may create weak joints. There is no universal profile.
Optical inspection checks visible alignment and solder defects. X-ray can examine hidden DRAM joints, but electrical testing is still needed. Looks can deceive.
Verify the SPD Hub programming, PMIC output rails, memory continuity, and module operation under controlled conditions. A board may look fine and still fail at startup.
Records of materials, stackup, placement, reflow, inspections, and test results support later troubleshooting. They cannot prevent every intermittent fault, but they help narrow the search.
The Memory module manufacturing process begins with a design that defines the module’s layout and electrical requirements. A DDR5 DIMM uses 288 pins and is organized into two independent 32-bit subchannels. Its multilayer printed circuit board must be fabricated with carefully controlled impedance so high-speed signals can travel reliably between the memory components and the system.
During assembly, DRAM chips, an SPD hub, and a power management integrated circuit are mounted using surface-mount technology and reflow soldering. The SPD profiles are then programmed, and the module’s nominal 1.1 V supply is verified. Final testing checks capacity, timing behavior, and signal integrity, including operation at data rates of 4,800 MT/s and above. These design, assembly, programming, and validation steps help ensure that each module meets its intended performance and reliability requirements.
Velmix